
Electronics rarely fail for exotic reasons. In an EMS failure analysis laboratory the same mechanisms return again and again: cracked solder joints, electrochemical migration, electrostatic discharge and electrical overstress, conductive anodic filament growth inside the laminate. What differs is where they come from — design, process, or the field — and how cheaply they could have been prevented. This article summarises what Aurightec’s laboratory sees, how root causes are actually found, and which low-cost decisions prevent the most expensive field failures.
Paul Zhang, Director — Production, Engineering and Digitalization
Which failure mechanisms occur most often?
Aurightec’s laboratory has investigated nearly all of the classic mechanisms, with one exception: tin whiskers have been comparatively rare in its experience. In terms of frequency, solder joint cracks and ESD/EOS damage are the most common, typically appearing around twice a year. The remaining mechanisms — electrochemical migration, CAF, the popcorn effect and similar — appear roughly once every two years.
That distribution matters for prevention: the two most frequent mechanisms are also among the cheapest to design out, as the last section shows.
Design, process, or environment? Where failures come from
Sorting a failure into one of three origins is usually the fastest route to a fix, because each origin has a different owner.
Design-related failures
- Mechanical stress fractures — components placed too close to board-edge stress zones
- CAF — insufficient via-to-via spacing
- Poor solder joints and tombstoning — a process window too narrow for the design
Process-related failures
- Voids and poor solder joints — improper reflow profile
- Solder balls and bridging — poor stencil design or print quality
- Electrochemical migration — insufficient flux cleaning
- Popcorn effect — inadequate component baking
Field- and environment-related failures
- Corrosion and electrochemical migration — high-temperature, high-humidity operating environments
- Stress fractures — drops, vibration, or excessive insertion and extraction force
- ESD/EOS — electrostatic discharge or electrical overstress in use
- Tin whisker growth — accelerated under certain temperature and humidity conditions
Case 1: electrochemical migration between adjacent pads
Symptom. Returned PCBA samples showed intermittent short circuits and increased leakage current.
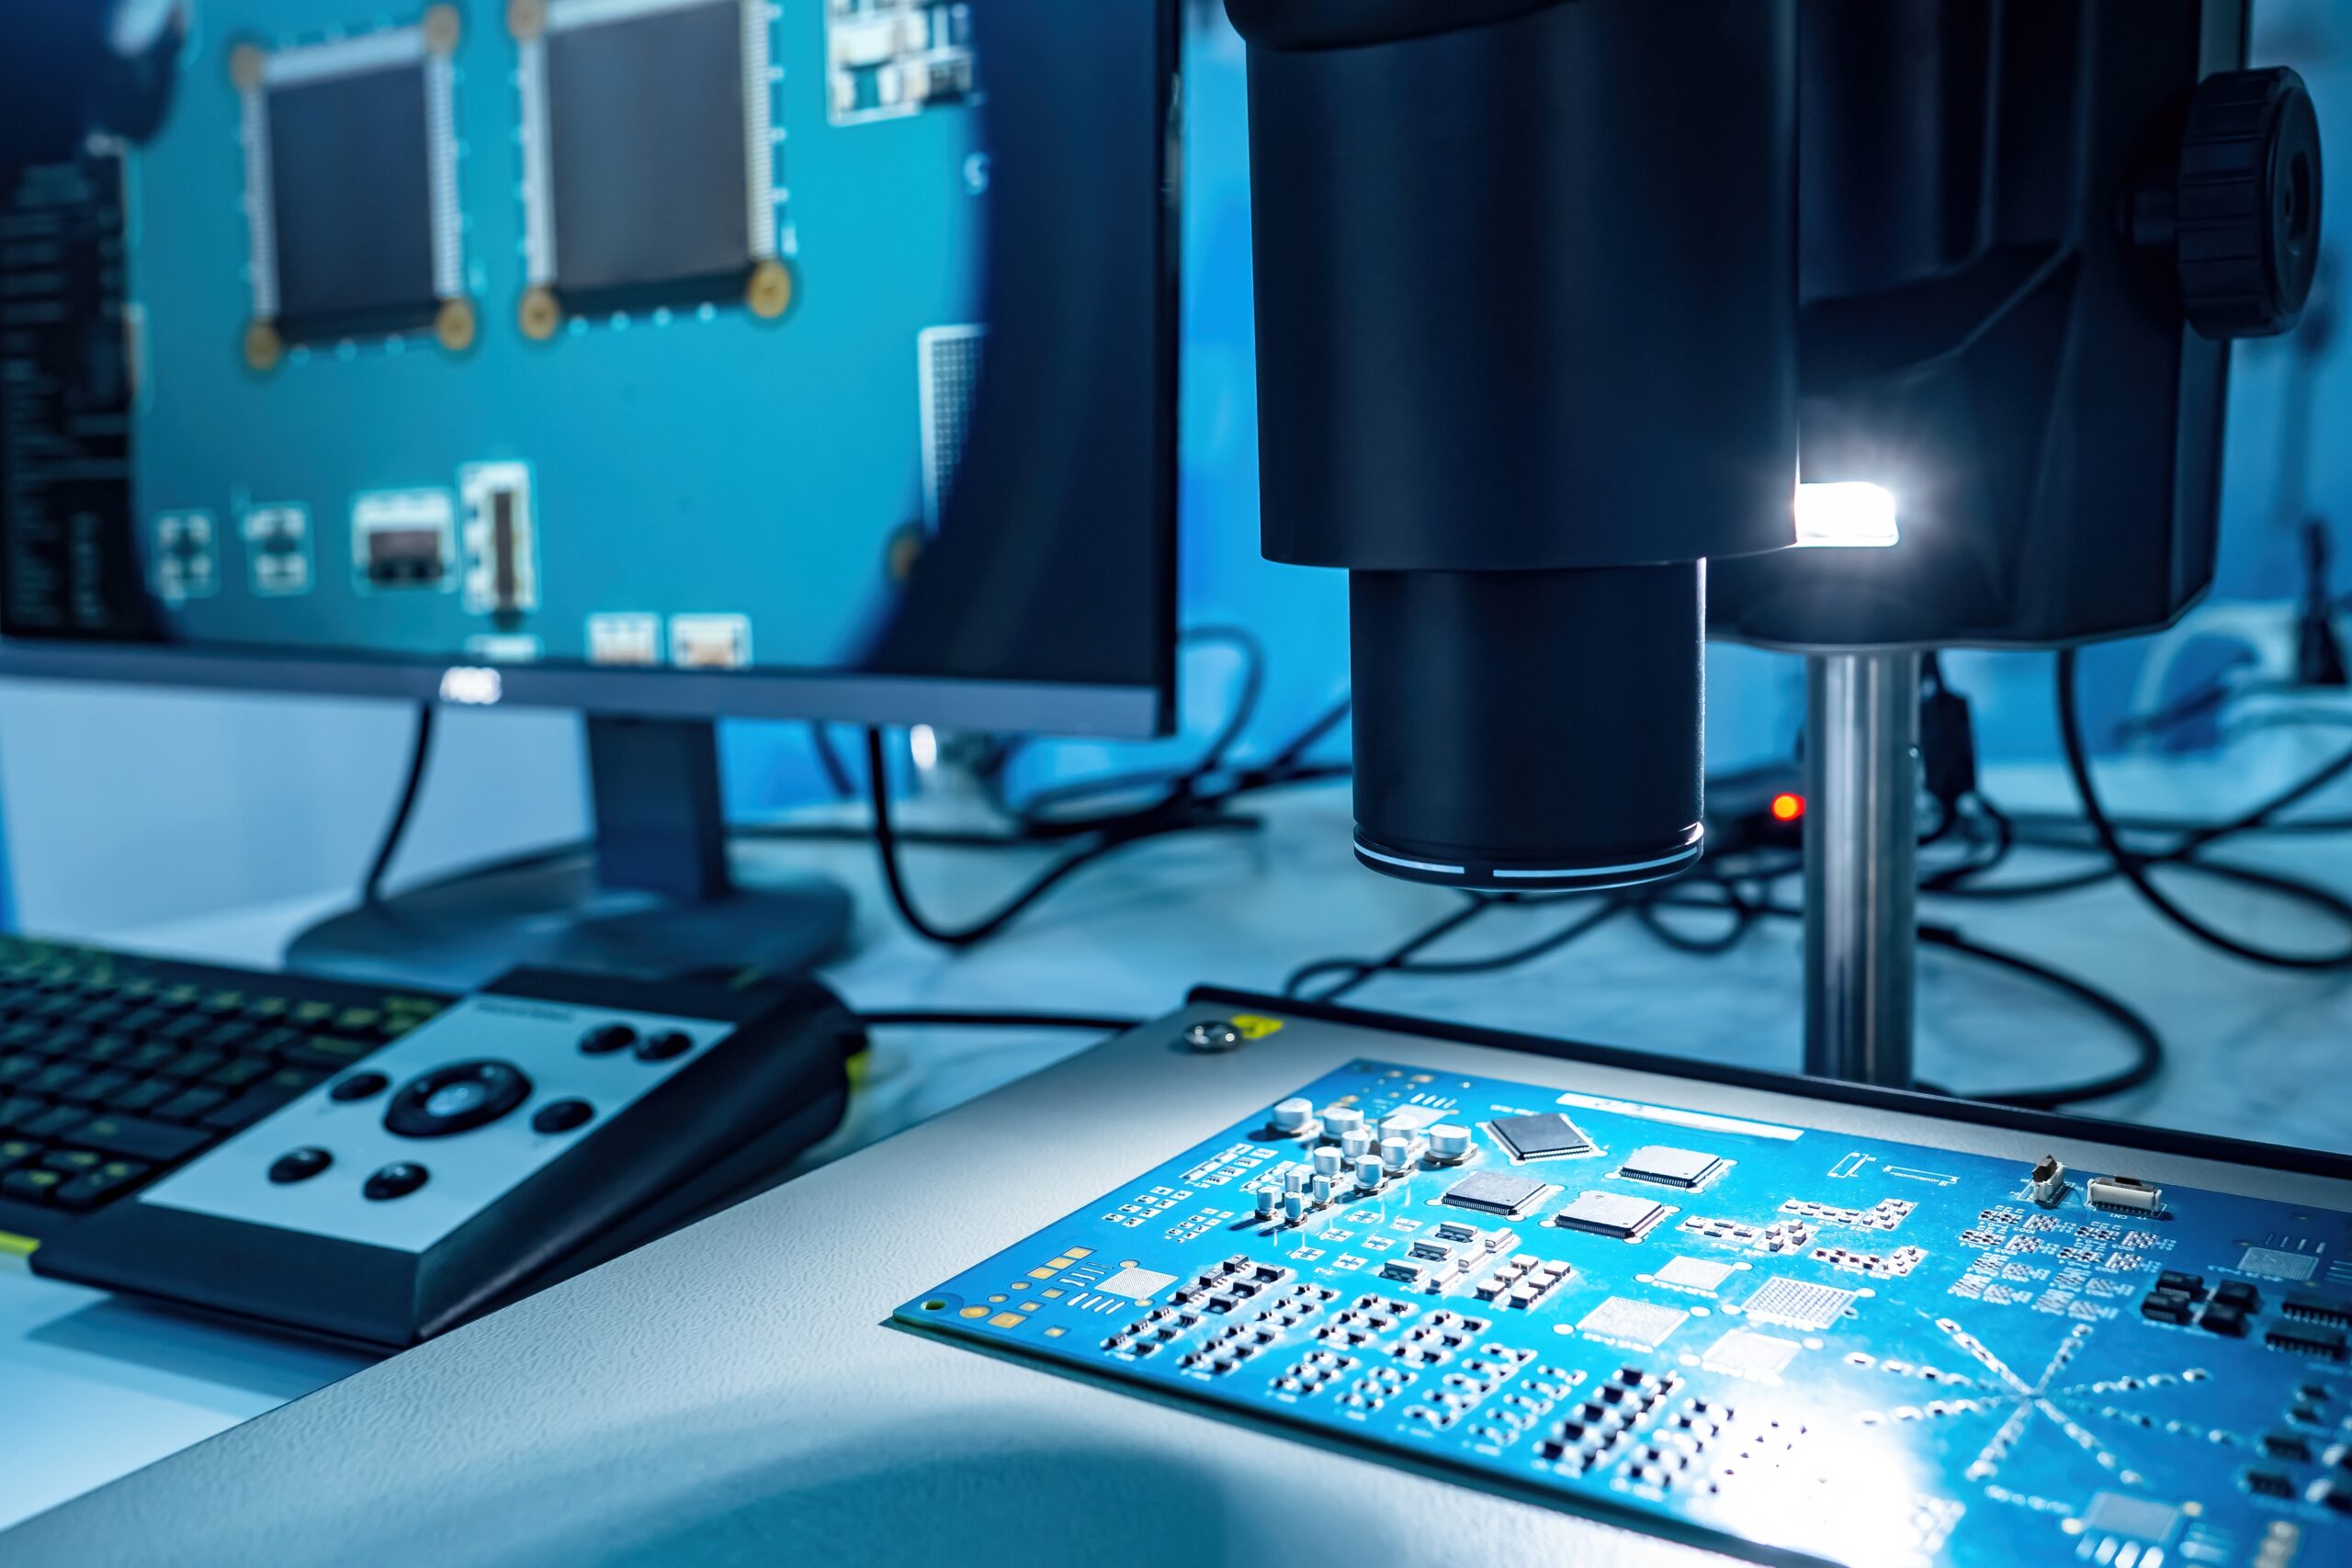
Investigation. Optical inspection revealed dendritic growth between neighbouring pads, with excessive flux residue in the affected area. SEM/EDS analysis confirmed the dendrites were composed of copper and tin. The mechanism was clear: flux residues plus moisture plus bias voltage produced electrochemical migration.
Corrective action. The cleaning process was improved to remove flux residues more thoroughly, and the PCB layout was optimized by adding solder mask dams between adjacent pads — increasing both physical spacing and creepage distance.
Case 2: conductive anodic filament (CAF) growth inside the PCB
Symptom. Insulation resistance dropped and intermittent shorts appeared on a board operating in a high-temperature, high-humidity environment. The failure was traced to adjacent plated through-holes in a dense layout area.
Investigation. Cross-section analysis of the failed area revealed filament-like conductive paths growing along the glass fibres inside the PCB laminate. SEM/EDS identified copper as the primary material in the filament.
Corrective action. The customer implemented two design changes: increased spacing between adjacent plated through-holes, lengthening the migration path, and a switch to laminate material with better anti-CAF performance.
Both cases share a pattern worth noting: the laboratory identified the mechanism, but the durable fix was a design change made together with the customer.
How electronics failure analysis is actually performed
Failure analysis follows one governing principle: non-destructive methods first, then semi-destructive or destructive methods when needed. Once a sample is cross-sectioned, it cannot be un-sectioned.
- Visual inspection. A high-power optical microscope examines the failed area for visible evidence — cracks, burn marks, corrosion, foreign particles. Almost every investigation starts here.
- X-ray inspection. Reveals internal structure without destroying the sample: solder voids, bridging and misalignment in BGA and QFN packages, and internal PCB trace fractures.
- Cross-section analysis. The sample is embedded in resin, cured, ground and polished — the most direct way to see solder joint internals, IMC layer morphology, crack paths and void distribution.
- SEM/EDS. Scanning electron microscopy gives high magnification and depth of field for fracture surfaces and corrosion products; EDS identifies the elemental composition of small areas, which traces contamination back to its source.
- Ion chromatography. Quantifies ionic residues on the PCBA surface — chloride, bromide, sodium, ammonium — the residues that drive electrochemical migration and corrosion.
The cheapest decisions that prevent the most expensive failures
Prevention splits between the design side and the process side. None of the measures below is expensive; all of them prevent failures that are.
On the design side
- Derate components against their maximum ratings. This alone prevents capacitor breakdown, resistor burnout, overvoltage damage and thermal runaway.
- Choose PCB and component surface finishes deliberately. The right finish prevents tin whiskers, poor SMT wetting and oxidation.
- Provide adequate test-point access. It makes ICT and functional test practical in manufacturing and raises test coverage — which is how defects are caught before shipment rather than in the field.
On the process side
- Comply with MSL handling per IPC/JEDEC J-STD-033. Prevents BGA "popcorn" cracking during manufacturing.
- Automate soldering where possible. Robotic or selective soldering instead of manual soldering improves through-hole barrel fill and overall solder joint reliability.
- Use no-clean soldering materials. Reduces the risk of electrochemical migration during field operation.
Frequently Asked Questions
What is the most common cause of PCB failure?
In Aurightec’s laboratory, solder joint cracks and ESD/EOS damage are the most frequently identified mechanisms — roughly twice a year each — while electrochemical migration, CAF and the popcorn effect appear around once every two years.
What is electrochemical migration (ECM)?
The growth of conductive metal dendrites between adjacent conductors under the combined influence of contamination (typically flux residue), moisture and bias voltage. It shows up as intermittent shorts and rising leakage current, and is prevented with thorough cleaning, adequate spacing and creepage distance, and no-clean materials.
What is CAF (conductive anodic filament)?
A conductive filament that grows along the glass fibres inside a PCB laminate, usually between closely spaced plated through-holes in humid conditions. It causes insulation resistance to drop and intermittent shorts. Prevention: greater via-to-via spacing and anti-CAF laminate material.
What is the popcorn effect in BGA components?
Cracking caused by moisture trapped inside a component vaporising during soldering. It is prevented by correct moisture-sensitivity-level handling and baking per IPC/JEDEC J-STD-033.
Investigating a field failure or a yield problem? Our laboratory finds root causes — and helps design them out.
Let’s talk